FY-PCM01
FY-PCM01 · Portable CNC cutter
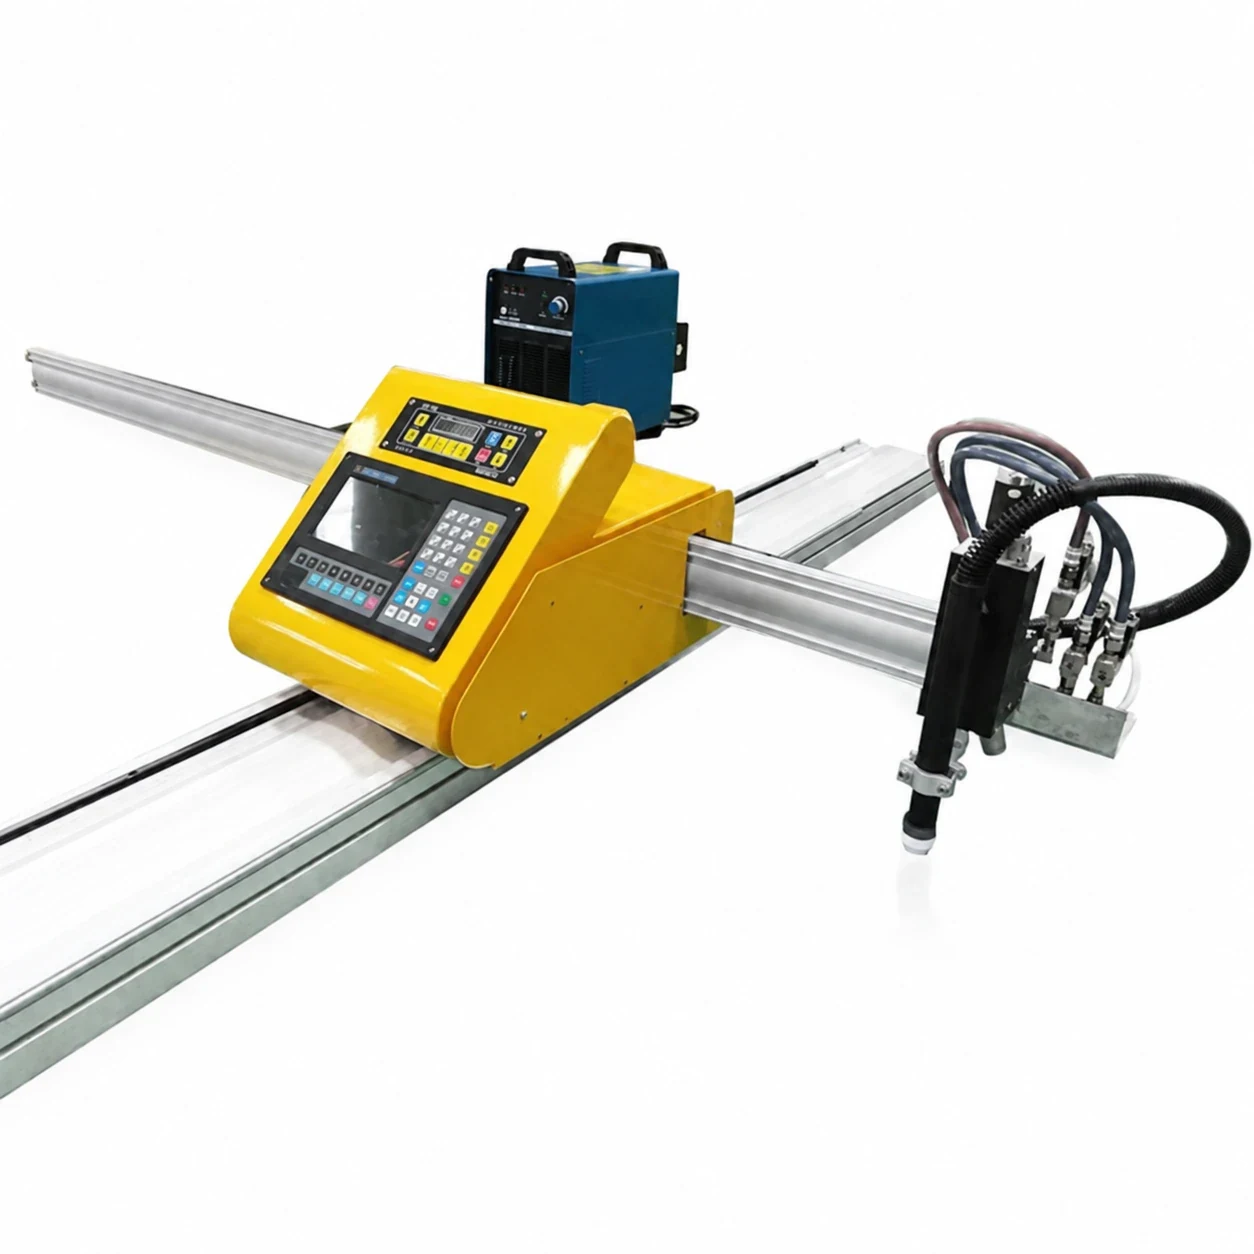
Portable format with configurable cutting area. The supplied sheet gives a 1500 × 3000 mm effective-area reference and also describes custom sizes.
View product ↗Compare FY-PCM01, FY-TCM01 and FY-GCM01 for CNC plate cutting. Specify plasma for suitable conductive-metal cutting, oxy-fuel for appropriate carbon-steel work, or a confirmed dual-process torch arrangement.
Source product image. Final configuration and included accessories are confirmed in the quotation.
Match the equipment to the material, part and production workflow.
Portable format with configurable cutting area. The supplied sheet gives a 1500 × 3000 mm effective-area reference and also describes custom sizes.
View product ↗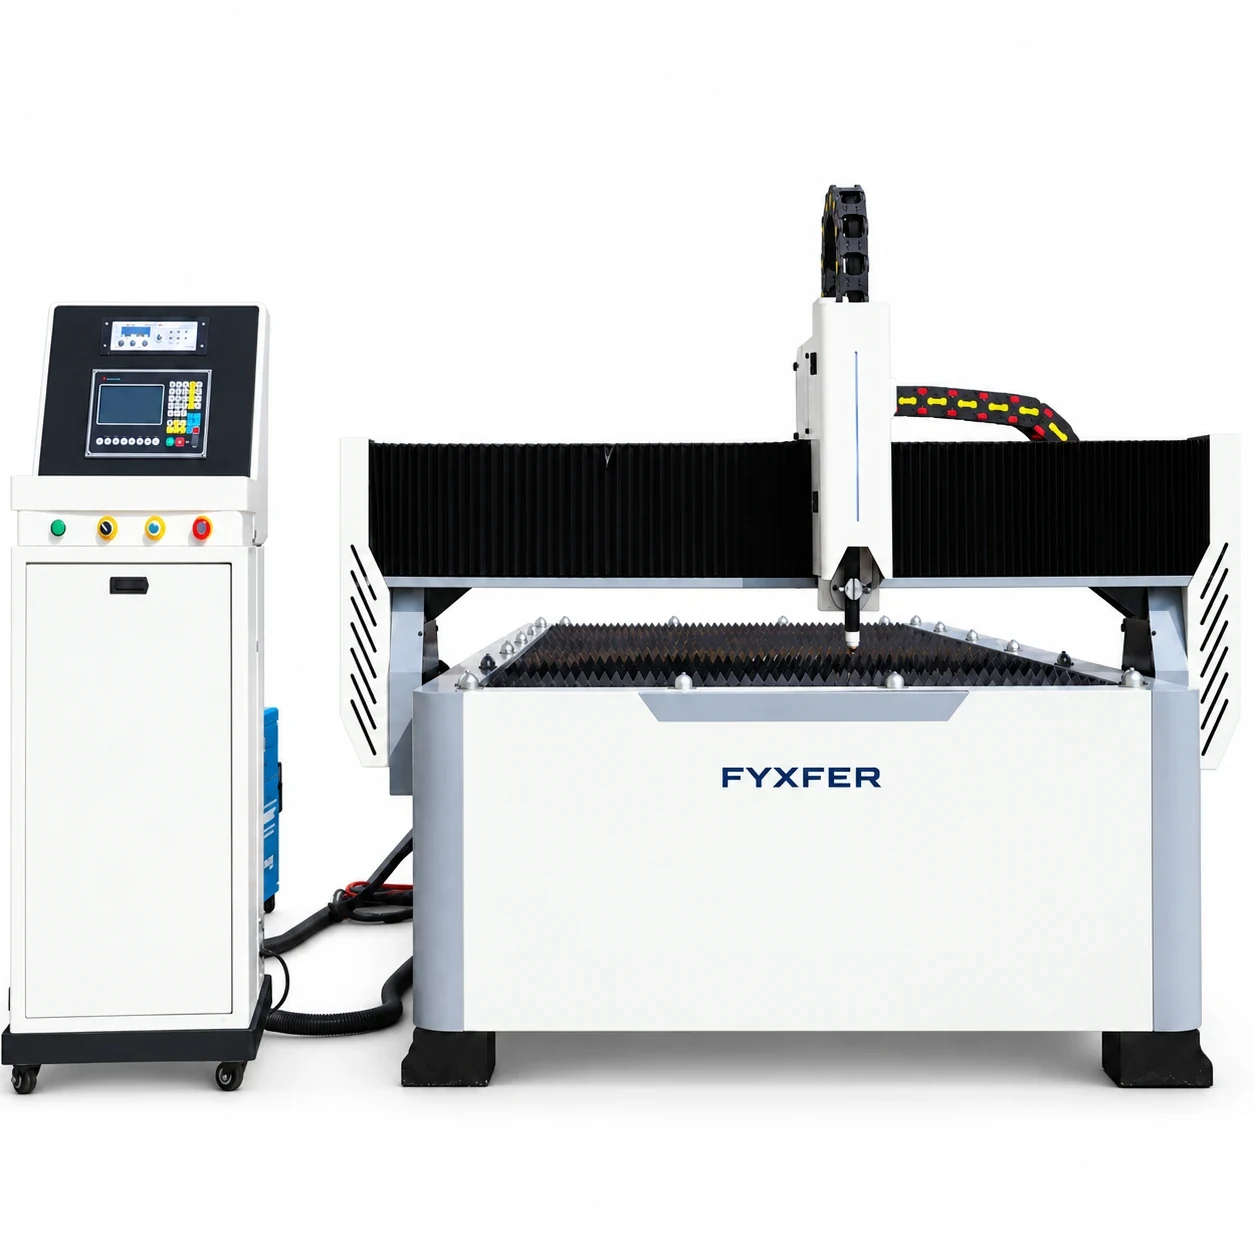
Steel plate-welded table format. The supplied sheet lists a basic 1500 × 3000 mm cutting area with sizes according to the application.
View product ↗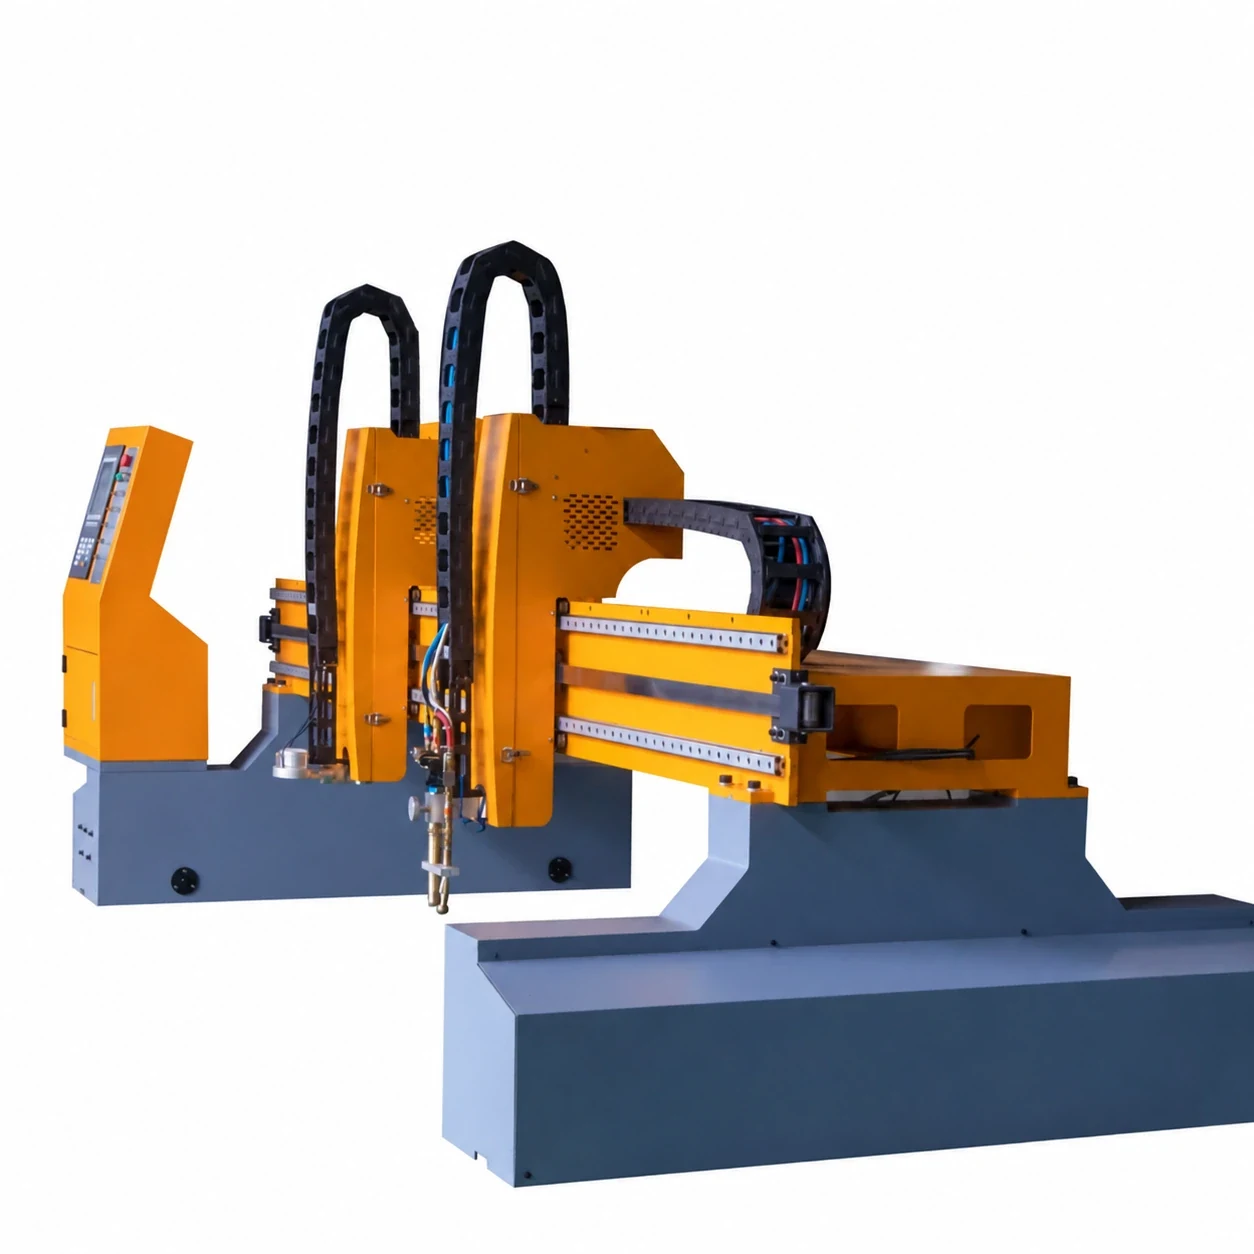
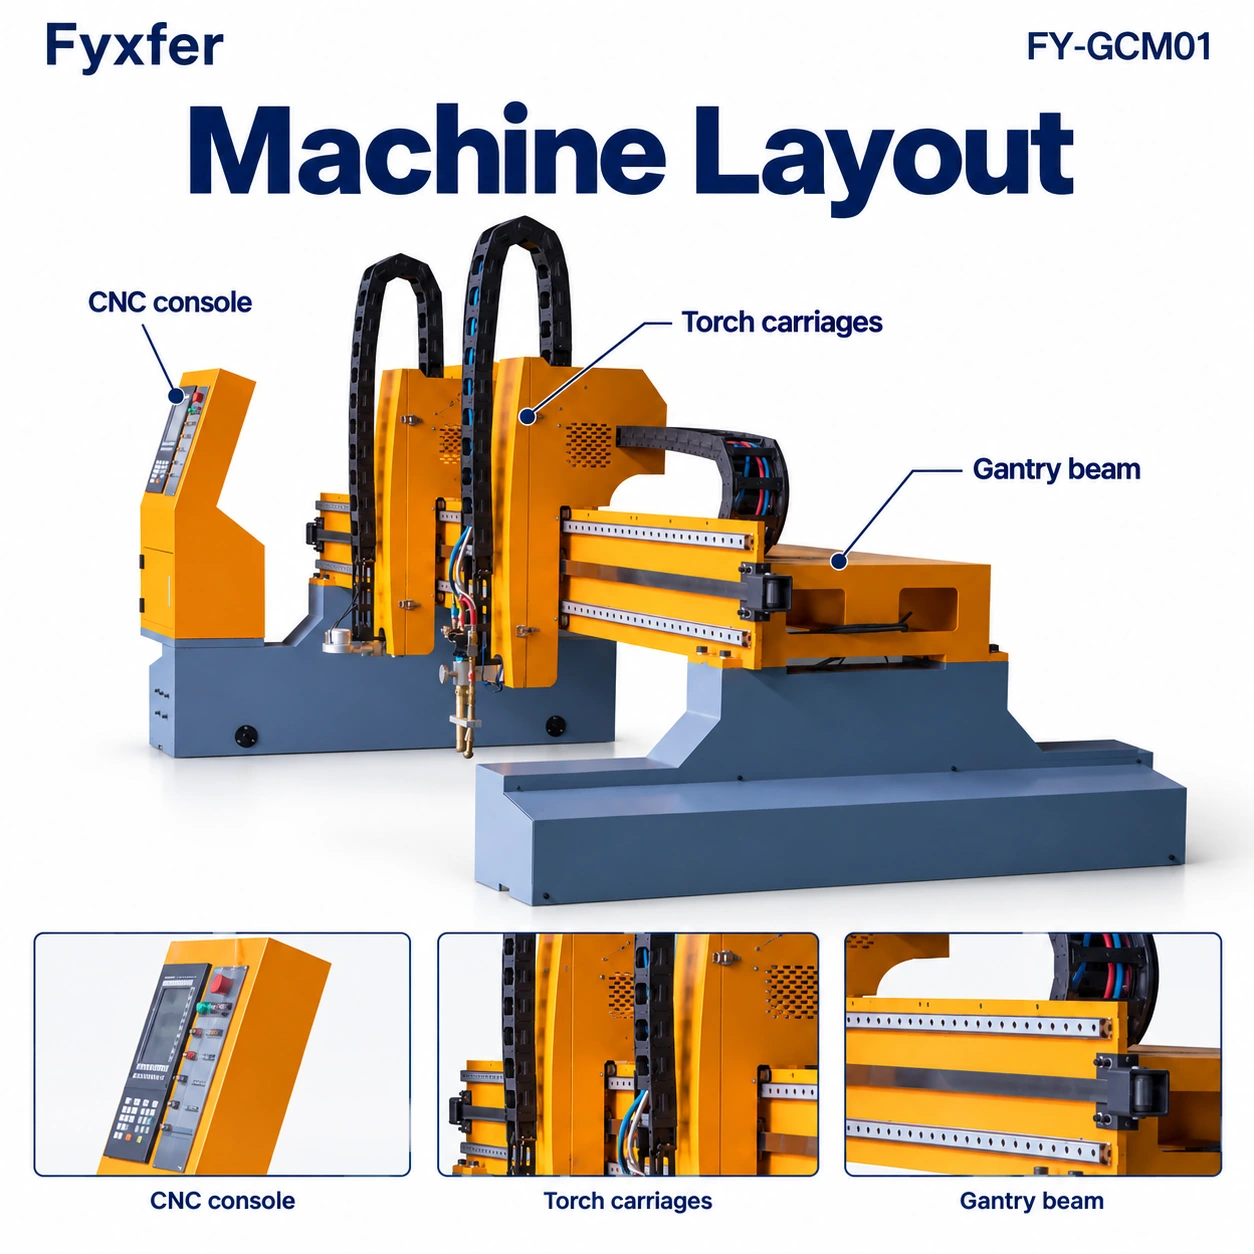
Steel plate-welded gantry format. The supplied reference configuration lists 2200 × 6500 mm cutting area within a 3000 × 8000 mm machine/rail layout.
View product ↗Confirm the final equipment and configuration in the quotation.
Plasma cuts electrically conductive materials. Carbon steel, stainless steel and aluminium require the appropriate source, current, gas/air setup and consumables. Ask for the matched cut chart and sample edge quality.
Oxygen and fuel-gas cutting is principally selected for suitable carbon-steel work. Confirm the fuel, oxygen supply, nozzle, ignition and preheat arrangements.
Match the equipment to the material, part and production workflow.
Product photographs show supplied reference configurations. Plasma sources, controller brands, torches and site-built support items are confirmed in the final bill of supply.
Product photographs show supplied reference configurations. Plasma sources, controller brands, torches and site-built support items are confirmed in the final bill of supply.
Portable format with configurable cutting area. The supplied sheet gives a 1500 × 3000 mm effective-area reference and also describes custom sizes.
Confirm track layout, support table/foundation, controller and plasma power source. Controller, machine weight and transport dimensions depend on the selected configuration.
Steel plate-welded table format. The supplied sheet lists a basic 1500 × 3000 mm cutting area with sizes according to the application.
Confirm table layout, material supports, water/extraction arrangement, torch package, controller and plasma-source specification.
Steel plate-welded gantry format. The supplied reference configuration lists 2200 × 6500 mm cutting area within a 3000 × 8000 mm machine/rail layout.
Confirm effective area separately from overall layout, plus rails, foundations, lifting access, drive package and plasma/flame torches.
Source product image. Final configuration and included accessories are confirmed in the quotation.
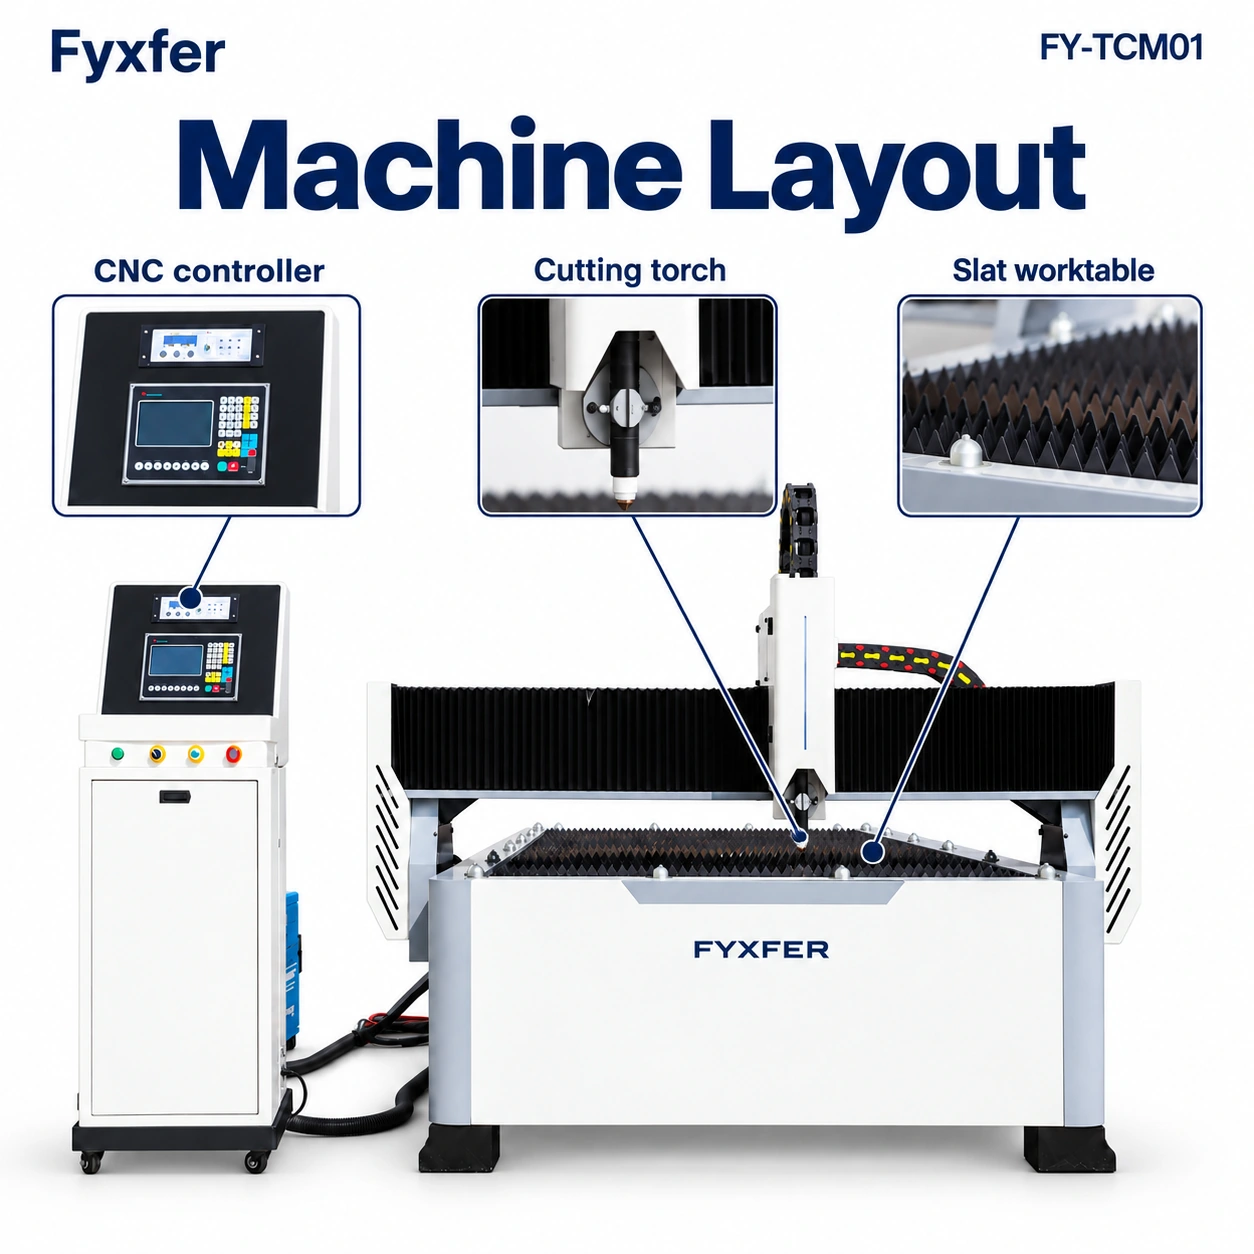
Explore the machine layout. Open each image at full size to read the labels.
Explore the machine layout. Open each image at full size to read the labels.
FY-TCM01 · Machine layout Illustrated layout; component appearance follows the quoted configuration. Open full-size image ↗
Technical process reference: Hypertherm plasma versus oxy-fuel . This reference describes processes; it is not certification of a particular FYXFER configuration.
Technical process reference: Hypertherm plasma versus oxy-fuel . This reference describes processes; it is not certification of a particular FYXFER configuration.
Plasma cuts electrically conductive materials. Carbon steel, stainless steel and aluminium require the appropriate source, current, gas/air setup and consumables. Ask for the matched cut chart and sample edge quality.
Do not use a power source’s maximum severance figure as its normal production or piercing capacity.
Oxygen and fuel-gas cutting is principally selected for suitable carbon-steel work. Confirm the fuel, oxygen supply, nozzle, ignition and preheat arrangements.
Conventional oxy-fuel cutting is not the general-purpose process for stainless steel or aluminium. Compare plasma or fiber laser for those jobs.
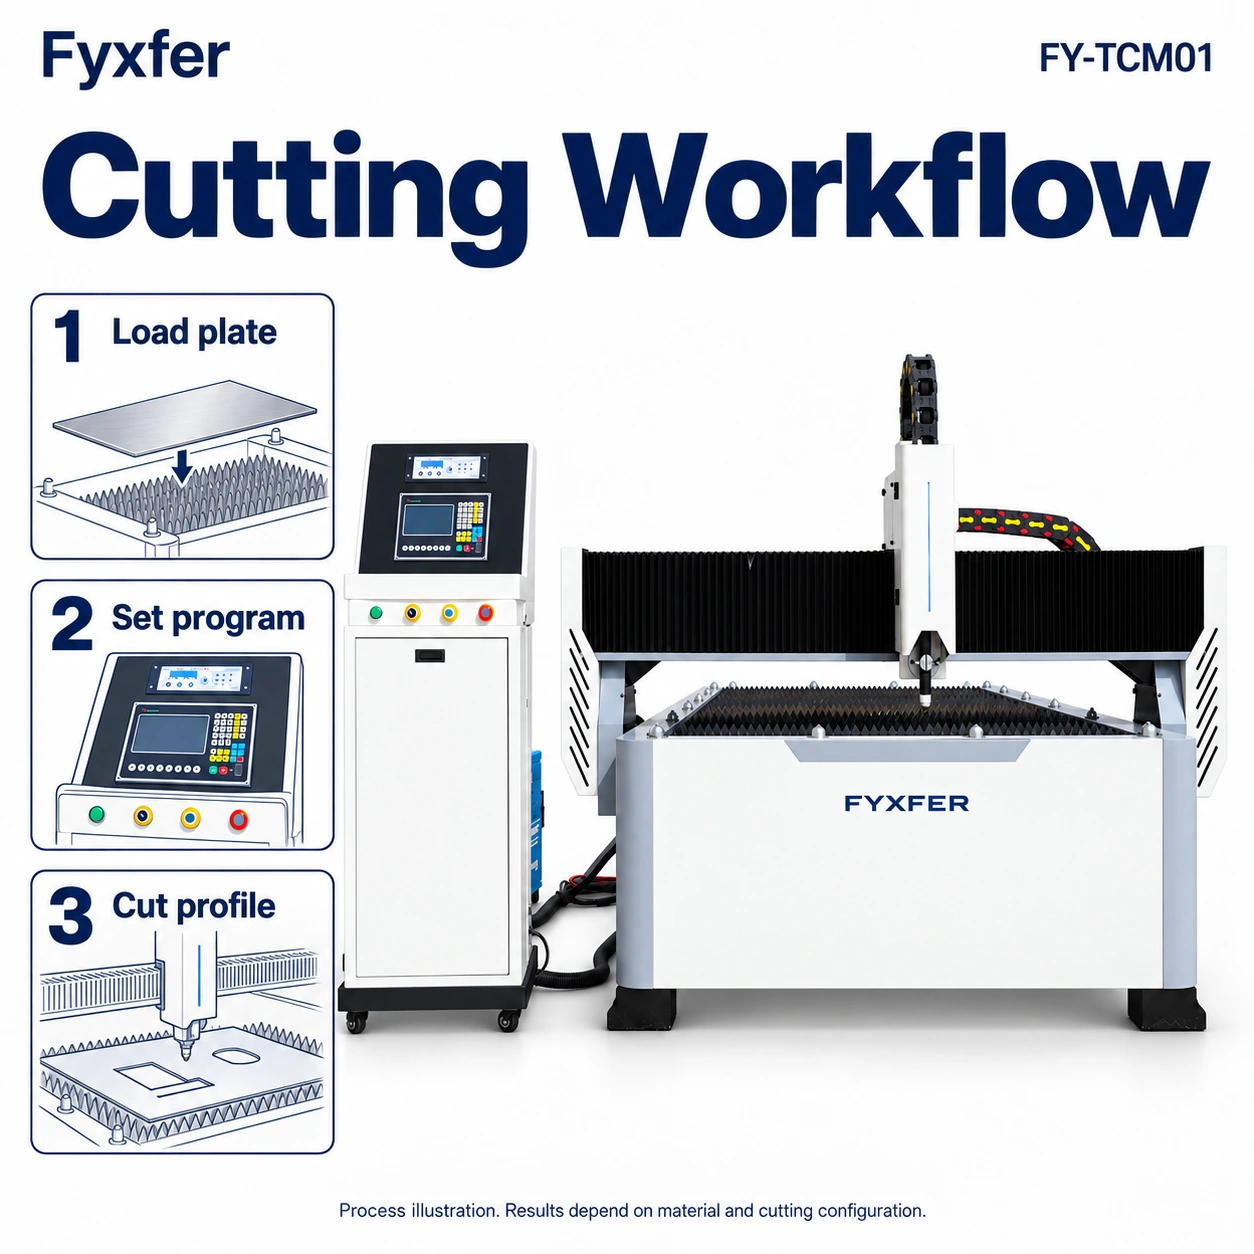
FY-TCM01 · Process concept Conceptual process illustration, not a cutting-test sample or operating procedure. Open full-size image ↗
Confirm the final equipment and configuration in the quotation.
| FY-PCM01 | Portable | 1500 × 3000 mm; custom sizes described | Rails, support structure, controller, source and torch package |
|---|---|---|---|
| FY-TCM01 | Table | 1500 × 3000 mm basic reference; custom sizes described | Bed, material support, water/extraction arrangement, source and controls |
| FY-GCM01 | Gantry | 2200 × 6500 mm in the supplied reference configuration | Span/travel, foundation, rail installation, loading and torch layout |
Source: the corresponding FY-PCM01, FY-TCM01 and FY-GCM01 model sheets. Specify production thickness, edge-quality requirements and the selected power source when requesting a cutting-performance chart.
| Model | Format | Documented effective-area reference | Order-specific confirmation |
|---|---|---|---|
| FY-PCM01 | Portable | 1500 × 3000 mm; custom sizes described | Rails, support structure, controller, source and torch package |
| FY-TCM01 | Table | 1500 × 3000 mm basic reference; custom sizes described | Bed, material support, water/extraction arrangement, source and controls |
| FY-GCM01 | Gantry | 2200 × 6500 mm in the supplied reference configuration | Span/travel, foundation, rail installation, loading and torch layout |
Product photographs show supplied reference configurations. Plasma sources, controller brands, torches and site-built support items are confirmed in the final bill of supply.
Portable format with configurable cutting area. The supplied sheet gives a 1500 × 3000 mm effective-area reference and also describes custom sizes.
Confirm track layout, support table/foundation, controller and plasma power source. Controller, machine weight and transport dimensions depend on the selected configuration.
Steel plate-welded table format. The supplied sheet lists a basic 1500 × 3000 mm cutting area with sizes according to the application.
Confirm table layout, material supports, water/extraction arrangement, torch package, controller and plasma-source specification.
Steel plate-welded gantry format. The supplied reference configuration lists 2200 × 6500 mm cutting area within a 3000 × 8000 mm machine/rail layout.
Confirm effective area separately from overall layout, plus rails, foundations, lifting access, drive package and plasma/flame torches.
Explore the machine layout. Open each image at full size to read the labels.
Technical process reference: Hypertherm plasma versus oxy-fuel . This reference describes processes; it is not certification of a particular FYXFER configuration.
Plasma cuts electrically conductive materials. Carbon steel, stainless steel and aluminium require the appropriate source, current, gas/air setup and consumables. Ask for the matched cut chart and sample edge quality.
Do not use a power source’s maximum severance figure as its normal production or piercing capacity.
Oxygen and fuel-gas cutting is principally selected for suitable carbon-steel work. Confirm the fuel, oxygen supply, nozzle, ignition and preheat arrangements.
Conventional oxy-fuel cutting is not the general-purpose process for stainless steel or aluminium. Compare plasma or fiber laser for those jobs.
Source: the corresponding FY-PCM01, FY-TCM01 and FY-GCM01 model sheets. Specify production thickness, edge-quality requirements and the selected power source when requesting a cutting-performance chart.
| Model | Format | Documented effective-area reference | Order-specific confirmation |
|---|---|---|---|
| FY-PCM01 | Portable | 1500 × 3000 mm; custom sizes described | Rails, support structure, controller, source and torch package |
| FY-TCM01 | Table | 1500 × 3000 mm basic reference; custom sizes described | Bed, material support, water/extraction arrangement, source and controls |
| FY-GCM01 | Gantry | 2200 × 6500 mm in the supplied reference configuration | Span/travel, foundation, rail installation, loading and torch layout |
Site-built rails, supports, air/gas lines and utility work appear as customer-prepared items in some source configurations. Confirm responsibility for every item rather than assuming a turnkey package.
Compare machine formats and process requirements for plasma and oxy-fuel cutting projects.
FY-PCM01 · FY-TCM01 · FY-GCM01
PDF · English · 114.5 KB FYXFER_Plasma_Oxy_Fuel_Selection_Guide_EN.pdf
Confirm the selected equipment, fixtures, utilities, installation needs and supply scope before ordering.
A portable CNC plate-cutting format with configurable working area. Choose the process for your material, then confirm tracks, plate support, controller, source and torch equipment rather than assuming a complete site-ready package.
Confirm the final equipment and configuration in the quotation.
Review carbon steel, stainless steel or aluminium with a suitable plasma source, consumables and accepted edge requirement.
Evaluate oxy-fuel for appropriate carbon-steel work, with the fuel, oxygen, nozzle and preheat arrangement defined.
Consider the portable format where track placement and plate support need to be configured around the work area.
Match the equipment to the material, part and production workflow.
Define the effective cutting area and how the plate is supported before choosing a portable format. Tracks, foundations and support structures can involve customer-prepared work; portable does not specify transport weight or remove installation requirements.
No. The documented 1500 x 3000 mm dimension is an effective-area reference. Confirm track layout, support and operating access separately.
Confirm the final equipment and configuration in the quotation.
Plasma and oxy-fuel are different processes, not interchangeable torch labels. Review the material and production thickness, then select a source and torch package with an appropriate cut chart and sample edge requirement.
Conventional oxy-fuel is not the general-purpose choice for those materials. Review a matched plasma or fiber-laser process instead.
Confirm the final equipment and configuration in the quotation.
Confirm the controller, file workflow, torch height control and source, along with electricity, air or gas and consumables. A clear responsibility list makes quotations comparable even when the portable platforms look similar.
It is not the normal production or piercing capacity. Request the selected source cut chart and compare representative parts under agreed conditions.
Confirm the final equipment and configuration in the quotation.
Confirm the final equipment and configuration in the quotation.
| Model and format | FY-PCM01; portable CNC cutting format. |
|---|---|
| Effective cutting area | 1500 x 3000 mm documented reference; custom sizes described. |
| Track and support | Track layout, support table and foundation confirmed in the project scope. |
| Cutting process | Plasma, oxy-fuel or a confirmed dual-process arrangement; not automatically all included. |
| Controller and source | Selected CNC controller and plasma-source specification stated in the quotation. |
| Torch and controls | Torch package, height control, ignition and file workflow confirmed for the chosen process. |
| Site services | Air/gas quality, electricity, earthing and extraction reviewed for the installation. |
| Transport and performance | Weight, packing dimensions, thickness and cutting performance depend on the selected configuration. |
Do not assume so. Some documented configurations assign rails, supports and utility work to the customer; confirm every responsibility.
Compare FY-TCM01 if your project calls for a dedicated table arrangement. Match effective area, plate support and process scope before comparing prices.
Record material, thickness, source/current, gas, speed, start method and the agreed edge criteria for the selected configuration.
Mention FY-PCM01 and send material grade, thickness range, plate dimensions and drawings. Describe the cutting area, site support and whether plasma, oxy-fuel or both are required.
Continue on our contact page to share your application and request a configuration.
Discuss my application ↗A steel plate-welded table format for CNC plate cutting. Review the source, torch and plate-support arrangement with your material and workflow, then define water or extraction provisions and the equipment included in the order.
Confirm the final equipment and configuration in the quotation.
Assess profiles and components in suitable conductive metals using the selected source, current and consumables.
Review flame cutting where appropriate for the material and job, with fuel and oxygen arrangements confirmed.
Plan recurring plate work around the table, material supports, loading method and site extraction or water arrangement.
Match the equipment to the material, part and production workflow.
Start with stock size, plate weight and finished-part handling. The welded-table format establishes the machine arrangement, but the supports, loading route and water or extraction provisions must be specified for the project.
It is the documented basic cutting-area reference. Custom sizes are described, while overall footprint and process capacity require separate confirmation.
Confirm the final equipment and configuration in the quotation.
Identify the exact material and edge requirement, then compare a cut chart for the proposed plasma source or an appropriate oxy-fuel setup. Piercing, production cutting and maximum severance are different conditions.
No. Specify the normal production and starting conditions, then assess representative parts against the agreed quality rather than a maximum severance figure.
Confirm the final equipment and configuration in the quotation.
Review torch height control, ignition, controller language and drawing or nesting workflow alongside the physical table. Agree what the supplier includes and what the workshop prepares, including power, air/gas and site works.
Inclusion depends on the final bill of supply. Confirm the source, controller, software workflow and installation items explicitly rather than inferring them from a photograph.
Confirm the final equipment and configuration in the quotation.
Confirm the final equipment and configuration in the quotation.
| Model and construction | FY-TCM01; steel plate-welded table CNC cutter. |
|---|---|
| Cutting area | 1500 x 3000 mm basic reference; application-specific sizes described. |
| Table support | Bed layout and material supports confirmed for the ordered configuration. |
| Cutting process | Plasma or appropriate oxy-fuel; dual-process torch arrangement requires confirmation. |
| Power source | Plasma-source specification, current range and matched cut chart agreed for the job. |
| Torch and controller | Process torch, controller, height control, ignition and file workflow itemised in the quotation. |
| Water and extraction | Selected arrangement and included equipment confirmed; neither assumed standard. |
| Site and acceptance | Electricity, air/gas, earthing, loading and sample criteria reviewed with the installation scope. |
No. It is principally for suitable carbon steel. Stainless steel and aluminium require review of a different process, such as matched plasma.
FY-TCM01 uses a welded table arrangement. Compare it with FY-PCM01 tracks and support requirements using the same workpiece, required area and utilities.
Confirm the effective area, table supports, source, torch, controller, consumables, water/extraction arrangement and supplier/customer responsibilities.
Mention FY-TCM01 and share plate size, material, thickness range and part drawings. Include your loading plan, edge requirement and preferred cutting process.
Continue on our contact page to share your application and request a configuration.
Discuss my application ↗A steel plate-welded gantry format for CNC plate cutting. Define effective cutting area separately from rails and overall layout, then review lifting access, foundations and the plasma or flame equipment required for your work.
Confirm the final equipment and configuration in the quotation.
Review stock dimensions, profiles and nested parts against effective width and travel rather than overall rail dimensions.
Assess suitable carbon steel, stainless steel or aluminium using the specified source, gas/air and consumables.
Consider appropriate oxy-fuel cutting with fuel, oxygen, nozzle, ignition and preheat requirements defined for the project.
Match the equipment to the material, part and production workflow.
The reference combines a 2200 x 6500 mm cutting area with a 3000 x 8000 mm machine/rail layout. Review span, travel and the surrounding site separately; neither dimension describes every custom installation.
No. It describes the supplied reference machine/rail layout. The documented effective cutting area is 2200 x 6500 mm.
Confirm the final equipment and configuration in the quotation.
Describe the stock, plate support and route used to load and remove parts. Rails, foundations, support items and installation responsibilities can materially change the project scope even when the nominal cutting area is unchanged.
Do not assume a turnkey site. Some documented configurations include customer-prepared items; confirm drawings, rail supply, foundations and installation responsibilities line by line.
Confirm the final equipment and configuration in the quotation.
Specify plasma, oxy-fuel or a confirmed dual-process arrangement. Match the source and consumables to production thickness, then agree sample conditions and edge criteria instead of using a maximum severance figure as normal capacity.
No. Plasma is selected for suitable conductive materials; conventional oxy-fuel is principally for appropriate carbon steel, not general-purpose stainless-steel or aluminium cutting.
Confirm the final equipment and configuration in the quotation.
Confirm the final equipment and configuration in the quotation.
| Model and construction | FY-GCM01; steel plate-welded gantry CNC cutter. |
|---|---|
| Effective cutting area | 2200 x 6500 mm in the supplied reference configuration. |
| Machine/rail layout | 3000 x 8000 mm reference; not the effective cutting area or a complete site-clearance plan. |
| Span and travel | Confirmed with rails, foundations and selected drive package. |
| Cutting processes | Plasma, flame or confirmed dual arrangement; exact torches specified in the quotation. |
| Source and controls | Plasma source, controller, height control and ignition package confirmed together. |
| Site utilities | Air/gas, electricity, earthing, extraction and plate supports reviewed for the project. |
| Supply and performance | Foundation/rail drawings, lifting access, consumables and sample acceptance agreed; no universal speed or thickness assigned. |
Compare FY-TCM01 when its table arrangement fits the work. Use the same required cutting area, handling method and process package for a meaningful comparison.
Ask for the selected source specification and cut chart, distinguishing production cutting, piercing and severance conditions for your material.
Identify material, thickness, source/current, gas, speed and start method, with the drawing and quality criteria used to accept the part.
Mention FY-GCM01 and provide plate sizes, material, thicknesses and drawings. Include the required effective area, rail/foundation plan, lifting access and cutting-process preference.
Continue on our contact page to share your application and request a configuration.
Discuss my application ↗Start with your material and application. Add the dimensions, result and production target when known.
Continue on our contact page to share your application and request a configuration.
Discuss my application ↗